
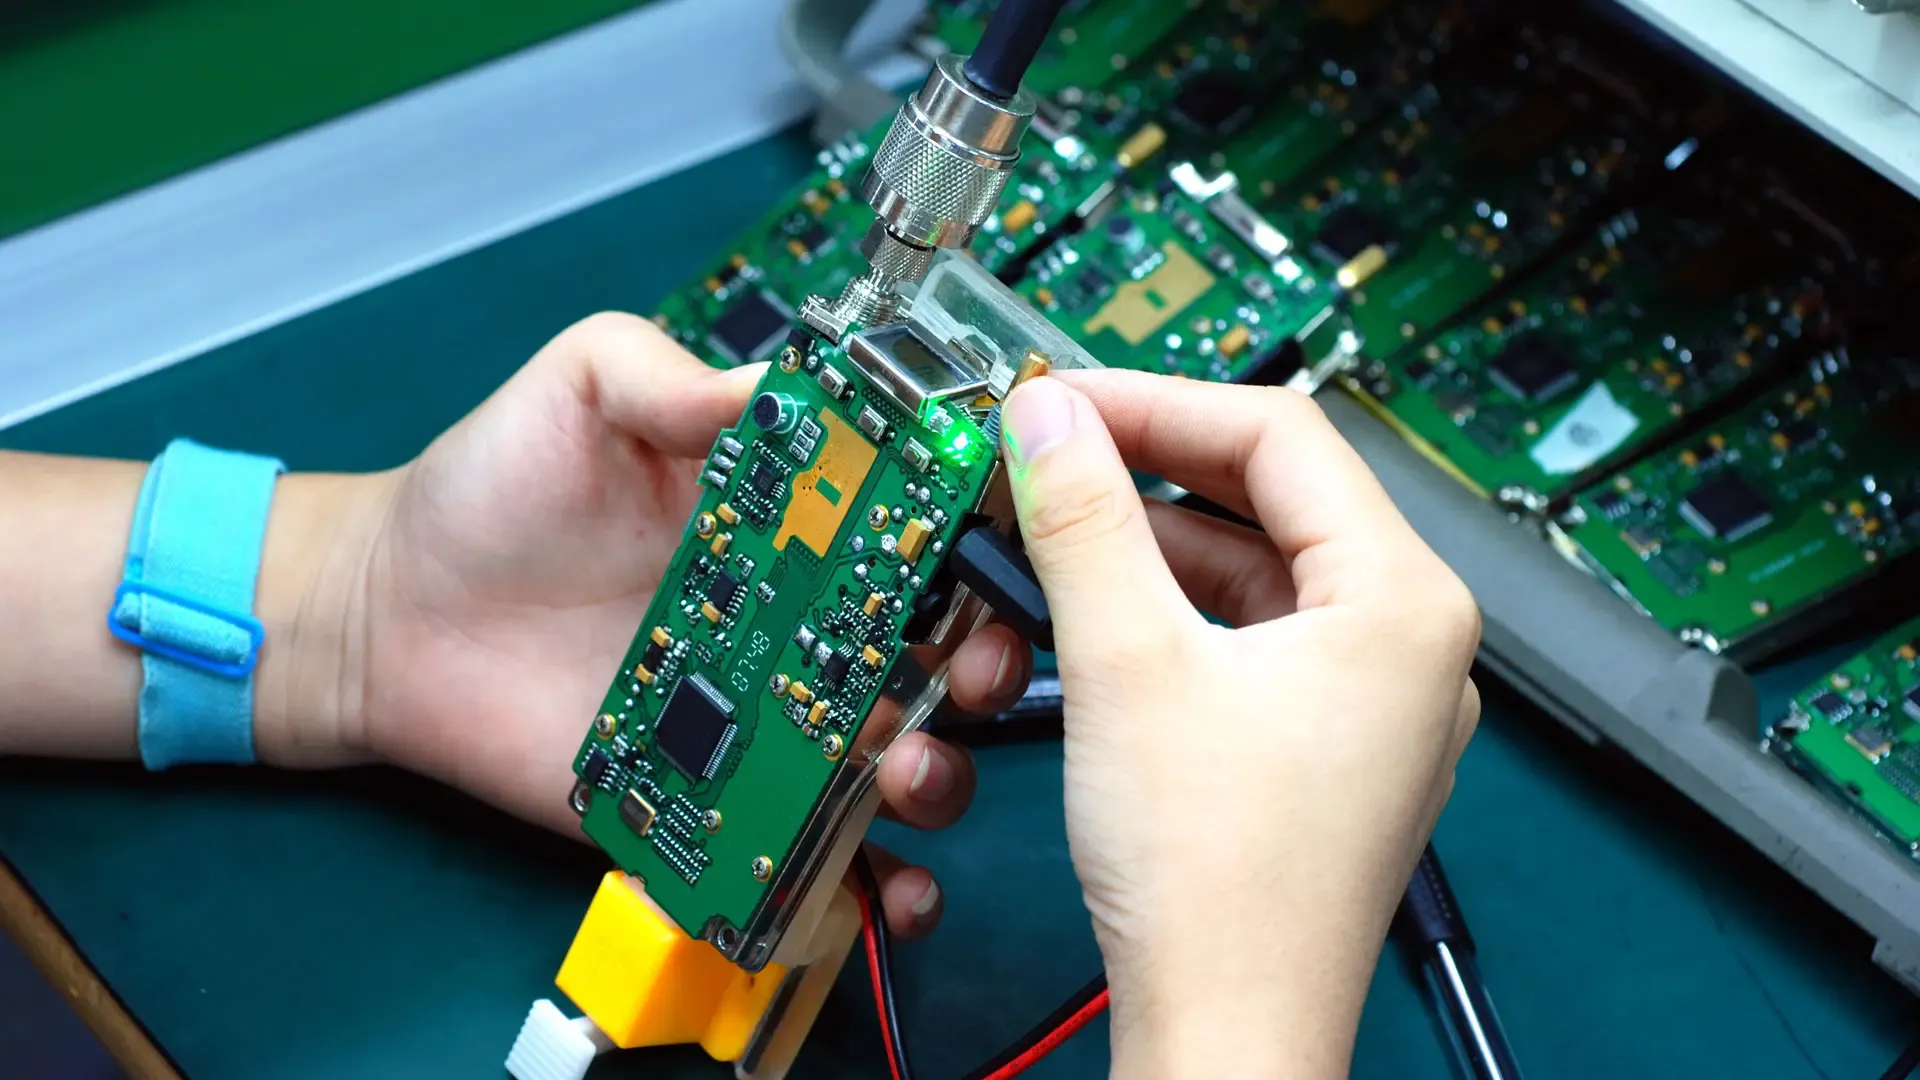
Direct Answer
Functional test is needed because AOI checks visible assembly quality, while functional test verifies that power, firmware, interfaces, sensors, outputs, and product behavior meet the required pass criteria.
Decision Model
Decision rule: Functional test is needed because AOI checks visible assembly quality, while functional test verifies that power, firmware, interfaces, sensors, outputs, and product behavior meet the required pass criteria. Treat the answer as release-ready only when the affected files, assumptions, and acceptance evidence are visible before quote.
Why It Matters
Explain the difference between visual inspection and product behavior verification. Late discovery changes cost, schedule, yield, or acceptance evidence after engineering and procurement have already made assumptions.
Engineering Principles
- Start from the engineering risk the question is trying to remove, not from a preferred keyword or default process.
- Explain the difference between visual inspection and product behavior verification. The answer should change at least one released input, review step, supplier responsibility, inspection scope, or acceptance expectation.
- If the same design files, stackup notes, BOM, inspection scope, and test plan would be sent either way, keep the answer as an FAQ on the closest entity page instead of publishing a standalone question.
Example
AOI may confirm that a connector is soldered; functional test confirms the board communicates through that connector.
Comparison
Use a comparison page when the decision is really between two named materials, finishes, packages, inspection methods, or sourcing models. Keep this page focused on the single question above.
RFQ Inputs
- released fabrication and assembly files
- revision, quantity, lead time, and allowed alternates
- materials, surface finish, stackup, inspection, and test requirements affected by this decision
- the reason why is functional test needed if aoi passes? changes the quote or manufacturing review
FAQ
What should be checked before quote?
Confirm source files, revision, materials, stackup, BOM, inspection scope, test requirements, quantity, and lead time before treating the answer as release-ready.
When should this become part of the RFQ?
Add it to the RFQ when the answer changes fabrication, sourcing, assembly, inspection, test, or delivery responsibility.
Can this replace a fabrication drawing?
No. It is a decision guide; the released drawing, BOM, and assembly notes remain the controlling documents.
Source Notes
- IPC standards source boundary - IPC official resources (standard).
Source fact: IPC official resources are used to locate standards context and public summaries, while paid standard text remains outside the repository. Omini interpretation: Use this to separate standards-backed engineering framing from copied acceptance criteria or unsupported numeric claims. Allowed usage: Use when a page needs IPC context but does not have a narrower public source registered yet.
- Existing OminiPCB repository content (internal): May seed structure and internal links; engineering claims still need external verification when specifications are involved.
CTA
Request a PCB quote when the design files and acceptance requirements are ready for engineering review.
Inspection and Process-Control Guide
For Why is functional test needed if AOI passes?, inspection should be designed from the defect mechanism backward. First identify what can fail, then select the method that can observe that failure, define the acceptance rule, and record the evidence needed for containment. AOI, X-ray, electrical test, functional test, and visual inspection answer different questions; passing one does not prove that the others are unnecessary.
Match the Method to the Defect
| Risk | Useful evidence | Limitation to state in the purchase order |
|---|---|---|
| Solder bridges, missing parts, polarity, offset | SPI/AOI plus operator review | Hidden joints and some bottom-side features may not be visible |
| Voids, head-in-pillow, hidden BGA joints, bottom-terminated components | 2D or 3D X-ray with a defined sampling plan | Image interpretation and access depend on package and board geometry |
| Opens, shorts, wrong values, unpowered nets | Flying-probe or fixture-based electrical test | Test-point access and netlist quality control coverage |
| Firmware, communications, sensor or power behavior | Functional test with a controlled fixture | It cannot replace workmanship inspection or prove every net |
| Surface damage, contamination, marking and workmanship | Visual inspection against the agreed class and drawing | It depends on lighting, magnification, training and consistent criteria |
The supplier should identify the inspection stage, reference design revision, program revision, sampling plan, defect coding, and reaction plan. “100% inspection” is incomplete unless the buyer knows what is inspected, at what resolution, and how false calls and escapes are handled.
Release Package
- Approved Gerber or ODB++/IPC-2581 data and a revision-controlled drawing.
- BOM with manufacturer part numbers, approved alternates, polarity and DNI status.
- Assembly drawing with critical-to-function references.
- Test points, programming interface, fixture boundary, and pass/fail limits.
- Workmanship class and acceptance standard agreed before the first build.
- Required reports: inspection summary, defect Pareto, rework log, electrical-test result, and traceability record.
Root-Cause Questions
When a defect is found, do not immediately increase inspection. Ask whether the error entered through the stencil, paste condition, placement program, feeder setup, reflow profile, component variation, laminate distortion, or operator rework. A useful corrective action changes the process control that created the defect and verifies the change on a subsequent lot.
Practical FAQ
Is visual inspection enough?
Only when the risk is visible and the assembly has no hidden, electrical, or functional requirement that needs another method.
Should every board receive X-ray?
Decide from package type, defect consequence, process capability, and customer requirements. Document the scope rather than using X-ray as an undefined label.
What should be requested after a pilot run?
Request defect Pareto, rework causes, inspection coverage, first-pass yield, test failures, and open corrective actions. These are more useful than a pass/fail statement alone.