Direct Answer
HDI PCB design uses laser-drilled microvias, fine traces, and sequential lamination to route high-pin-count BGA packages within tight form factors. By planning via types, stackup symmetry, and material constraints early, you can reduce fabrication cost and avoid reliability failures. This guide explains HDI from a manufacturing perspective, helping you make stackup, via, DFM, and sourcing decisions that survive production.
Why HDI PCB Design Matters for Modern Electronics
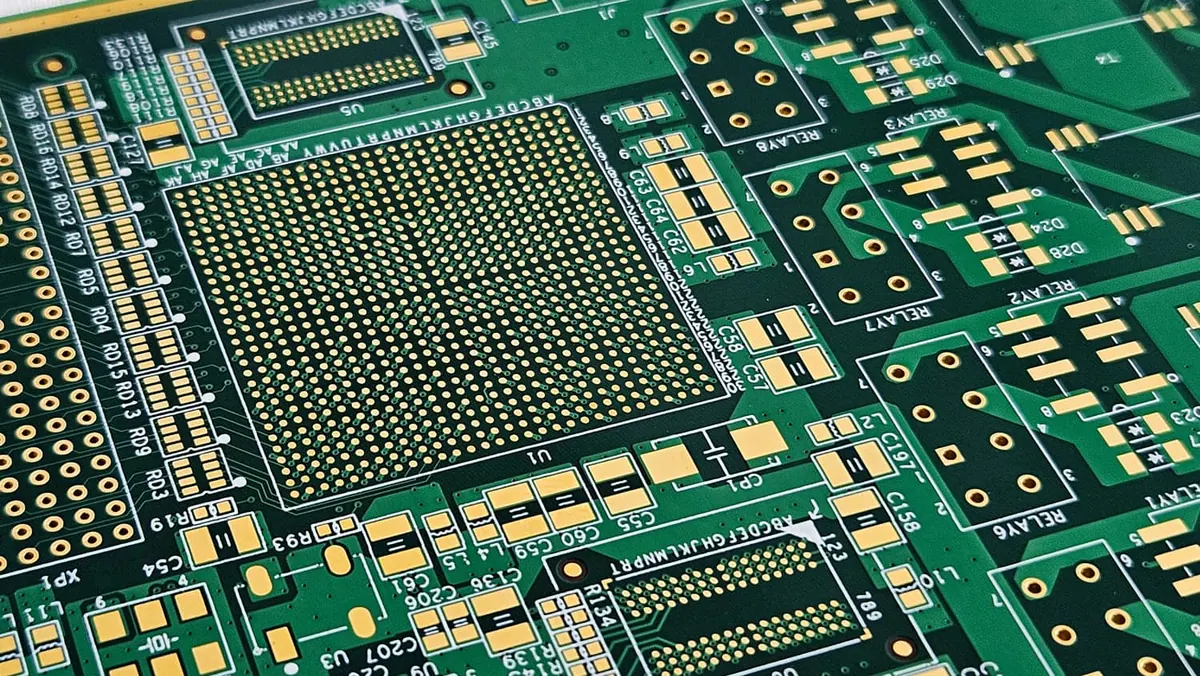
High-Density Interconnect (HDI) technology exists because conventional through-hole and standard multilayer boards cannot economically route the pin counts found on modern BGAs, QFNs, and chiplets. When a 0.4 mm pitch BGA has 500+ I/O, the escape routing density required exceeds what a traditional 8-layer board with 0.1 mm traces can deliver. HDI solves this by moving interconnection density from the drilled hole to the copper layer.
The Electrical Benefits Beyond Routing Density
HDI is not merely a routing convenience. Shorter signal paths between vias reduce parasitic inductance and capacitance, which directly improves signal integrity for high-speed interfaces like DDR4/DDR5, PCIe Gen4/5, and serializer/deserializer lanes. A microvia with a 0.075 mm drill diameter has roughly half the parasitic capacitance of a standard 0.2 mm plated through-hole in the same stackup. That difference matters at 10+ Gbps signaling rates where every femtofarad contributes to impedance mismatch and jitter.
The power integrity story is similar. Via-in-pad for decoupling capacitors places the bypass cap directly under or adjacent to the power pin, minimizing loop inductance. For mixed-signal designs, HDI lets you keep analog and digital reference planes intact by avoiding drilled vias that punch through solid copper.
When HDI Is the Right Choice
You should consider HDI when any of the following conditions apply:
- You have a BGA with 0.4 mm or smaller pitch.
- Your board area is constrained (e.g., wearables, handheld devices, medical probes).
- Your design requires via-in-pad for decoupling or thermal management.
- You need to reduce layer count by using microvia escape routing instead of blind/buried vias on standard layers.
- Your differential pairs require impedance control below 100 Ω with tight tolerance (±5%).
Conversely, if your board has 0.65 mm or larger BGA pitch, fewer than 200 nets, and 4–6 layers of routing space, standard multilayer manufacturing is more economical. HDI adds lamination cycles and laser-drilling steps, which increases base cost before you even consider yield.
HDI Stackup Planning: The Engineering Foundation
The stackup is the single most important decision in HDI design. It determines via types, lamination count, material selection, and final cost. A poorly planned stackup often forces a redesign because the via architecture you chose cannot be manufactured or fails impedance requirements.
HDI Build-Up Types and Lamination Cycles
IPC-2226 (the HDI-specific design standard) classifies HDI boards by build-up structure. From a manufacturing perspective, the key variable is the number of sequential lamination cycles. Each lamination cycle adds cost, lead time, and yield risk.
| HDI Type | Structure | Lamination Cycles | Typical Use Case |
|---|---|---|---|
| Type I | Microvias on one or both outer layers, no buried vias | 1 additional cycle | Consumer wearables, simple BGA breakout |
| Type II | Microvias on both outer layers + buried vias | 2 additional cycles | Mid-complexity BGA routing |
| Type III | Microvias on both outer layers + buried vias + at least two layers of buildup | 3+ additional cycles | High-pin-count BGAs, advanced SIPs |
| Any-Layer | Microvias connect any layer to any other layer | Multiple cycles | High-end servers, AI accelerators |
Each lamination cycle introduces thermal expansion stress. If your stackup is asymmetric (e.g., 1+6+1 instead of 2+6+2), the board can warp after reflow. IPC-6012, the qualification standard for rigid PCBs, requires that fabrication meet warp and twist limits for the final assembled board. Asymmetric copper distribution across the build-up layers is the most common cause of field-level solder joint failure in HDI assemblies.
Material Selection for HDI
Standard FR-4 with Tg 130–140°C is insufficient for most HDI laminations because the repeated thermal cycles during sequential lamination degrade the resin system. Use at minimum a Tg 170 material (e.g., FR4-TG170) or a low-loss laminate (e.g., Isola 370HR, Panasonic Megtron 6) depending on your signal speed. The laminate must also be compatible with laser drilling; materials with high glass filler content can cause uneven via shapes or excessive residue at the via bottom.
For impedance control, note that the dielectric constant (Dk) of the prepreg used between buildup layers will shift after lamination. Design your differential pair spacing using post-lamination Dk values, not the raw material datasheet values. Many fabricators provide this data in their design guideline documents. If you are sourcing from a new manufacturer, always ask for their Dk/Df values used in their impedance calculation tools. IPC-4101 covers laminate material specification, but it does not dictate the specific Dk you should design to; that is a fabrication-specific decision.
Via Architecture: Microvias, Blind, Buried, and Via-in-Pad
The choice of via types directly controls routing density and manufacturing yield. Understanding the laser drill, plating, and filling processes helps you make decisions that reduce fabrication defects.
Microvia Geometry and Aspect Ratio
A microvia is laser-drilled with a typical drill diameter between 0.075 mm and 0.125 mm. The aspect ratio (depth to diameter) is limited by the capability of the laser drill to create a clean, platable via. For most fabricators, the practical limit is 1:1 for standard microvias; some high-end shops can achieve 1.5:1, but at higher cost and lower yield.
A common mistake is designing a microvia with a high aspect ratio to reduce capture pad size. The plating process (typically electroless copper followed by electrolytic plating) must uniformly deposit copper inside the via barrel. If the aspect ratio exceeds the plating bath's throwing power, the via barrel will have thin copper at the center, creating a latent reliability defect that only surfaces after thermal cycling. Design your stackup so that each microvia depth does not exceed the drill diameter.
Blind and Buried Vias: When to Use Them
Blind vias connect an outer layer to one or more inner layers, while buried vias connect inner layers only. These are mechanical-drilled and require more process steps than microvias. Blind vias are useful when you need to connect a BGA pad to an inner power plane without routing through the outer layer. Buried vias are useful for transferring signals between core layers when the outer layers are too dense for through-vias.
The critical design rule is via placement and capture pad size. For mechanical blind vias, the minimum annular ring (copper ring around the drilled hole) should be at least 0.05 mm on target for Class 2, and 0.075 mm for Class 3 per IPC-6012. For microvias, the capture pad (the copper pad on the target layer) should be at least the drill diameter plus 0.1 mm on each side. If you leave insufficient capture pad, the laser may not fully land on the copper, causing an open circuit or a microvia with a tapered sidewall that fails reliability testing.
Via-in-Pad: Design Rules for BGA and HDI Boards
Via-in-pad places a microvia directly inside a component pad, which is common for high-density BGA escape routing. The primary concern is solder joint integrity. When a via is not filled or plugged, solder wicks down the via barrel during reflow, leaving insufficient solder at the joint interface.
For via-in-pad, copper-filled vias (filled with electrolytic copper and then capped with flat copper) are the premium solution. The flat cap surface provides a solderable pad that matches the BGA ball diameter. See the detailed PCB Via-in-Pad Design Rules for BGA and HDI Boards for specific dimensional criteria. Rule of thumb: the filled via's copper cap must be flat within 0.025 mm to avoid solder ball voiding. For non-critical vias, conductive epoxy plugging is acceptable, but note that it increases resistance and is unsuitable for high-current paths.
DFM Rules Specific to HDI
Design for Manufacturability (DFM) is not a generic checklist; it must be tailored to the HDI processes you use. The number of defects in HDI is positively correlated with the number of laser drill shots, sequential lamination steps, and via fill operations. Each additional process step is an opportunity for misalignment, contamination, or plating voids.
Capture Pad Size and Placement
Your EDA tool's default via/pad settings are often designed for standard through-holes. For microvias, you must override these defaults. Use the following guidelines as a starting point:
- Microvia drill diameter: 0.075–0.1 mm
- Capture pad diameter: drill diameter + 0.15 mm (for outer layer) and + 0.1 mm (for inner layer)
- Non-solder mask defined (NSMD) pads are preferred over solder mask defined (SMD) for BGA and via-in-pad because they allow the router to adjust mask opening without hitting copper.
- Maintain a minimum spacing of 0.1 mm between via capture pads and adjacent copper features to avoid registration issues during sequential lamination.
Copper Weight and Trace Spacing
HDI emphasizes fine-line etching. The minimum trace/space you can achieve depends on the copper weight. For 1/2 oz copper (18 µm), most fabricators can reliably produce 0.075 mm (3 mil) lines and spaces. For 1 oz copper (35 µm), the minimum is typically 0.1 mm (4 mil). Attempting 0.075 mm traces on 1 oz copper causes under-etch along the trace edges, reducing the effective conductor width and potentially violating impedance tolerances.
When you specify impedance control, remember that the dielectric thickness between the trace and reference plane is the primary control variable. In HDI stackups, the prepreg thickness is often dictated by lamination cycles. You might need to adjust the reference plane distance by adding an extra prepreg ply to hit a 50 Ω single-ended impedance, which then affects the total board thickness. Always run impedance calculations after finalizing the stackup, not before.
Surface Finish Selection
The surface finish choice affects solderability, wire bonding (if used), and cost per square inch. For BGA pads, ENIG (electroless nickel immersion gold) provides good planarity but suffers from "black pad" risks when the immersion gold thickness is out of spec. ENEPIG is superior for both solderability and aluminum wire bonding, and it improves the reliability of the via-in-pad copper cap. For high-volume consumer products, immersion silver or OSP is cheaper but requires careful handling and is unsuitable for multiple reflow cycles. If your assembly cycles the HDI board more than once (e.g., for double-sided assembly with a heavy BGA side), choose ENIG or ENEPIG.
The DFM Review Process: Verifying Your HDI Design
A thorough DFM review before fabrication is the cheapest insurance against costly revision loops. Do not rely solely on your EDA tool's DRC; manufacturer DFM tools check for different constraints, such as via-to-copper clearance on inner layers, plating aspect ratio, and lamination symmetry.
Step-by-Step HDI DFM Checklist
- [ ] Verify microvia aspect ratio is within the fabricator's stated limit.
- [ ] Ensure the stackup is balanced: same number of layers and copper weight above and below the core.
- [ ] Check that microvia capture pads are at least 0.1 mm larger than the drill diameter.
- [ ] For via-in-pad, verify that the fill via has a flat cap and that the pad diameter accommodates the BGA ball.
- [ ] Run a simulation or manual check for lamination cycle count. Each additional cycle increases total board thickness slightly due to prepreg melt flow.
- [ ] Confirm that the specified material (e.g., FR4-TG170) and surface finish (e.g., ENEPIG) are available from your manufacturer; if you use a specific low-loss laminate, check the inventory lead time.
- [ ] Review the drill file to ensure no drill overlaps copper planes without adequate thermal relief (if required).
- [ ] Confirm impedance calculations use the manufacturer's Dk/Df values, not generic values from the laminate datasheet.
The RFQ Communication
Your RFQ must tell the manufacturer exactly what HDI features you need. Include:
- Layer count and total board thickness
- Build-up type (I, II, III, or any-layer)
- Via types and dimensions (microvia drill, blind, buried, through)
- Via-in-pad usage and spec (filled, capped, plated)
- Minimum trace/space and copper weight per layer
- Target impedance values and tolerance referencing specific differential pair groups
- Surface finish
- Material Tg/Dk value
- Reference to your specific PDF or ODB++ file version
Do not assume the manufacturer will infer via fill requirements. If you specify via-in-pad without "copper filled and capped", you will receive epoxy-filled vias at best, or worse, uncovered vias that cause solder wicking. State the requirement explicitly.
Practical HDI Design Example
Consider a 10-layer HDI board for an FPGA with a 0.5 mm pitch BGA, requiring 400 signal nets. The stackup is a 2+6+2 structure:
- L1–L2: Microvia layer pair (laser drilled), 0.075 mm drill
- L3–L8: Core layers with blind and buried vias
- L9–L10: Microvia layer pair (laser drilled)
The BGA pitch is 0.5 mm, so the pad diameter for NSMD is 0.25 mm, with a microvia capture pad of 0.2 mm on L2/L9. For the escape routing, the fan-out begins on L1; the microvia drops to L2, and then traces route horizontally on L2 before a buried via drops to L4. The top layer is used for 0.5 mm pitch BGA component placement and 0.4 mm pitch decoupling capacitors.
The impedance requirement is 100 Ω ±10% for DDR4 differential pairs. With Dk = 4.2 post-lamination, the differential trace width is 0.09 mm with 0.15 mm spacing, referenced to a solid ground plane on L3. But because L2 holds routing, the reference plane must be L3, creating a 0.2 mm dielectric gap. This causes the impedance to drop below 100 Ω, so you insert a 0.05 mm prepreg layer between L2 and L3 to bring the gap closer to the required value. That adjustment changes the total board thickness from 1.2 mm to 1.3 mm, which affects the mechanical enclosure clearance.
This example illustrates the iterative nature of HDI design: every via, layer, and dielectric thickness decision interacts. Use your manufacturer's design guidelines as a datasheet, not a suggestion.
Common HDI Mistakes and When to Involve the Manufacturer
Most HDI design errors are discovered at the fabrication stage, where they cause delays and cost overruns. By involving the manufacturer early — before the board is fully routed — you avoid redesign loops.
The most common mistakes are:
- Incorrect via stacking — stacking vias of different sizes directly on top of each other creates a "staircase" that is difficult to plate. Offset stacked vias slightly or use larger capture pads.
- Ignoring lamination cycles — designing a build-up structure that forces an extra lamination cycle unnecessarily inflates cost and lead time.
- Insufficient capture pads — relying on EDA default pads that are too small for laser registration.
- Aspect ratio violations — using a single microvia to span more than two layers.
- Ignoring symmetry — an unbalanced stackup with 4 layers above the core and 2 below normally warps after reflow.
- Over-specifying traces — requiring 0.05 mm traces on standard FR4 when the application only needs 0.075 mm, driving up cost without benefit.
- Forgetting via tenting — leaving inner-layer vias exposed can cause solder wicking or short circuits when the board is pressed.
When you hit a DFM violation that you cannot resolve with a minor layout change, contact the manufacturer. Ask specifically: "Is this via stack or capture pad size within your standard production capability, or does it require an engineering deviation?" A reputable manufacturer will answer honestly. For example, if your design needs an any-layer HDI structure and your volume is limited, the manufacturer may recommend a Type III structure to keep the lamination process manageable.
How HDI Affects Assembly, Inspection, and Reliability
HDI board assembly is not the same as standard SMT. The fine pitch and microvia content affect reflow profiling, X-ray inspection, and reliability modeling.
Reflow Profile and Moisture Sensitivity
HDI boards with multiple lamination cycles absorb moisture more readily at board edges and via barrels. Moisture trapped in the laminate vaporizes during reflow, causing delamination or "popcorn" voids at the via joints. Pre-baking the boards at 120°C for 2–4 hours before assembly is standard practice for HDI, in addition to any component-level MSL requirements. The solder paste stencil aperture for a 0.4 mm BGA is typically 0.2 mm, and paste deposition can vary; use a 3D SPI under 10 µm resolution to verify paste height within ±5%.
X-Ray Inspection Limits
Ordinary automated optical inspection (AOI) cannot see inside a microvia. X-ray inspection is required to verify barrel integrity, plating thickness, and the absence of voids in filled vias. However, X-ray throughput is lower than AOI, so it is usually applied to a sampling basis unless the assembly contract mandates 100% inspection for critical joints. If your design has 5,000+ microvias per board, factor inspection time into your production schedule.
Reliability Testing
IPC-6012 Class 2/3 boards are validated through thermal cycling and thermal stress tests. Unfilled microvias can pass initial electrical test but fail after 500 thermal cycles due to fatigue cracks at the via-to-pad interface. Filled and capped vias dramatically improve this failure mode because the copper cap redistributes stress. If your product specification requires 10-year field life, mandate copper-filled via-in-pad for all BGA pads. Do not substitute epoxy-filled unless you have qualified the board through a dedicated reliability test program.
For flex-to-rigid transition areas or HDI boards with thin cores (below 0.1 mm), consult the manufacturer about handling and support tooling during routing and assembly. The board may require a stiffener or a special carrier to avoid flexing during SMT placement. See the Flex PCB Manufacturing Process: An Overview for Beginners for how flexible materials behave differently during lamination and handling.
Sourcing Strategy and EMS Considerations
HDI boards are typically more expensive and longer lead time than standard PCBs. Your sourcing strategy should start during design, not after the Gerbers are finalized.
Panel Size and Utilization
HDI microvia drilling is a step-and-repeat process across a panel. Panel size influences cost: a 24 × 18 inch panel containing 25 copies of a 4 × 6 inch board is more cost-efficient than a 18 × 12 inch panel with 6 copies. Consider whether your board outline allows panelization without adding costly tabs or v-score lines that interrupt microvia rows.
EMS Integration
If you use an EMS provider for assembly, verify that their X-ray and AOI equipment can handle your via density and BGA pitch. A low-cost EMS using only 2D AOI will miss solder voids in via-in-pad joints. Ask for their inspection capability statement before signing a contract.
At Omini, we handle the full flow from DFM review through panelization, fabrication, and assembly. We recommend sending your stackup and via list in a structured format (e.g., IPC-2581 or ODB++) rather than only Gerber files, so the DFM check can validate lamination and via structure programmatically.
Before you submit your design, consider whether a standard 4-layer board with carefully planned blind vias could meet your constraints. If you are uncertain, refer to our practical overview of Decoding High-Density Interconnect (HDI) PCB Technology for a manufacturing-level comparison. For a broader view on how HDI fits into the total manufacturing workflow, our Circuit Board Manufacturing Process: A Practical Reference for Beginners covers the sequential steps from bare laminate through final electrical test.
FAQ: Common HDI Design Questions
1. Why is HDI PCB design important for modern electronics?
HDI allows higher component density, smaller form factors, and improved electrical performance by using microvias, fine lines, and multiple lamination cycles. It is essential for advanced BGA packages and portable devices where board area is a primary constraint.
2. What are common mistakes engineers make in HDI PCB design?
Common mistakes include incorrect via stacking, insufficient capture pad sizes, ignoring aspect ratio limits, and not considering the number of lamination cycles. These lead to fabrication defects, lower yields, and higher costs. For more detail, review the via-specific rules in our HDI design guidelines page: HDI PCB Design Comprehensive Guidelines.
3. How can I verify my HDI design before fabrication?
Run a thorough DFM check using your EDA tool and a manufacturer's DFM report. Verify via types, stackup symmetry, material availability, and surface finish compatibility. Share your stackup and via requirements in the RFQ.
4. What information should I include in an HDI PCB RFQ?
Include layer count, board thickness, material type (e.g., FR4-TG170), surface finish (e.g., ENEPIG), via types (microvia, buried, blind), minimum trace/space, and any impedance requirements. Also specify if via-in-pad is used and whether it will be filled and plated.
5. Does HDI always require via-in-pad?
No. Via-in-pad is only needed when the BGA pitch is too small to route a via between adjacent pads (typically below 0.5 mm pitch). For 0.5 mm and above, you can often route via between pads with a dog-bone fan-out pattern, which avoids the cost of via filling.
6. What laminate should I choose for an HDI board with high-speed signals?
For 10+ Gbps signals, use a low-loss laminate with a stable Dk across frequency, such as Panasonic Megtron 6 or Isola 370HR. For standard digital logic at lower speeds, FR4-TG170 is acceptable. Match the laminate to the maximum frequency, not the board thickness.
> Practical note: When you receive the manufacturer's DFM report, pay attention to the "via stacking" comments. If the fabricator flags your microvia capture pads as undersized, updating the pad diameter is a global change in your EDA tool — do it before panelization, not after.
> Engineering handoff note: HDI PCB Design: Comprehensive Guidelines, Process and Considerations, Flex PCB Manufacturing Process: An Overview for Beginners, and PCB Via-in-Pad Design Rules for BGA and HDI Boards before the release package is frozen.
> Also compare Decoding High-Density Interconnect (HDI) PCB Technology: An Overview and Circuit Board Manufacturing Process: A practical reference for Beginners before locking the quote scope.